| Typical alloy classification | Austenitic chromium-nickel stainless steel | Austenitic chromium-nickel-molybdenum stainless steel | Both grades are widely used for press-formed parts and can be stamped in annealed sheet or strip. |
| Carbon, maximum | 0.07 wt% | 0.07 wt% | Lower carbon helps reduce carbide precipitation during welding; it does not eliminate the need for suitable forming and joining procedures. |
| Chromium content | 17.5–19.5 wt% | 16.0–18.0 wt% | Chromium forms the passive oxide layer responsible for basic corrosion resistance. |
| Nickel content | 8.0–10.5 wt% | 10.0–14.0 wt% | Nickel stabilizes the austenitic structure and supports ductility during drawing and bending. |
| Molybdenum content | Not specified as a required alloying range | 2.0–3.0 wt% | Molybdenum improves resistance to localized corrosion, especially pitting and crevice corrosion in chloride-containing environments. |
| Tensile strength, minimum | 515 MPa (75 ksi) | 515 MPa (75 ksi) | The press, die, and blank-holder setup must withstand the forming load without excessive deflection. |
| Yield strength, minimum | 205 MPa (30 ksi) | 205 MPa (30 ksi) | Yield strength affects the force required to begin permanent deformation during stamping. |
| Elongation in 50 mm, minimum | 40% | 40% | High elongation supports stretching, bending, flanging, and moderate deep-drawing operations. |
| Brinell hardness, maximum | 201 HB | 217 HB | Hardness influences tool wear, springback, cutting force, and the press tonnage required. |
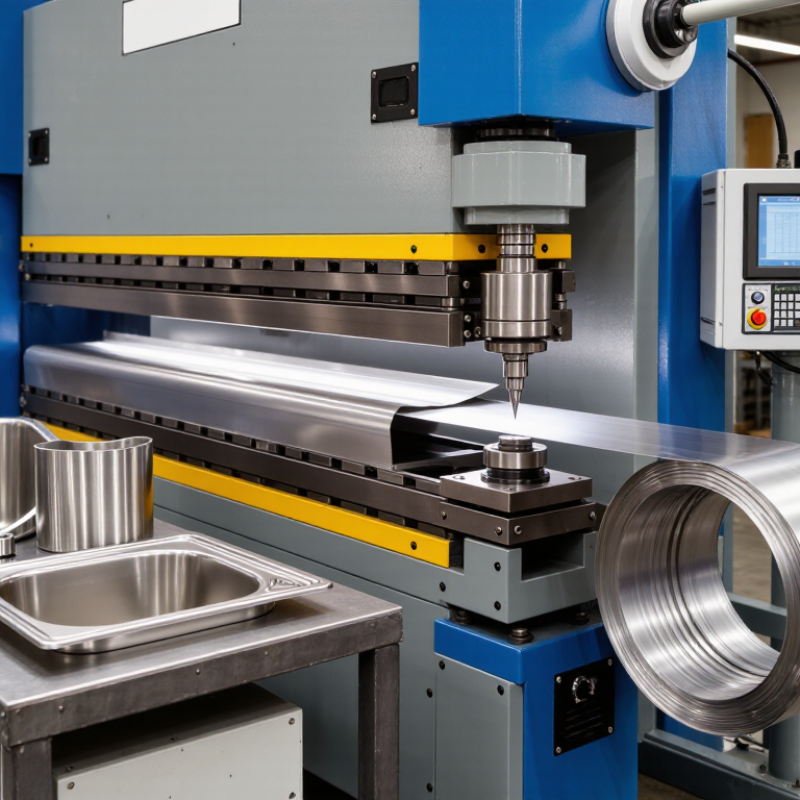
| Basic stamping sequence | Blanking → positioning → forming → piercing or trimming → inspection | Blanking → positioning → forming → piercing or trimming → inspection | A punch applies force to the sheet while the die supports and controls the material to create the designed geometry. |
| Common stamping operations | Blanking, bending, piercing, coining, embossing, flanging, and drawing | Blanking, bending, piercing, coining, embossing, flanging, and drawing | The operation is selected according to the required shape, dimensional tolerances, wall thickness, and production volume. |
| Work-hardening behavior | Significant work hardening during cold forming | Significant work hardening during cold forming | Progressive forming, adequate radii, proper lubrication, and intermediate annealing may be needed for demanding draw ratios. |
| General corrosion-resistance profile | Strong general atmospheric and many chemical-service resistance | Generally better resistance to chlorides and reducing chemical environments than Type 304 | Material selection should consider temperature, chloride concentration, exposure time, surface condition, and residual stresses. |
| Typical stamped-part applications | Brackets, covers, clips, housings, washers, kitchen components, and general fabricated parts | Chemical-processing components, marine-exposed parts, medical components, enclosures, and chloride-service hardware | The final grade should be selected from the service environment, forming requirements, cleanliness requirements, and applicable design specification. |

 Your message must be between 20-3,000 characters!