| Material Formulation | Compound selection should match the operating temperature, fluid exposure, ozone environment, dynamic loading, and required fatigue life. | ASTM D2000 may be used to classify rubber materials by physical properties and resistance requirements. | Polymer family, hardness range, tensile strength, elongation, compression set, temperature range, and fluid-resistance data. | Approved compound specification, material safety documentation, batch traceability, and certificate of analysis. | Critical |
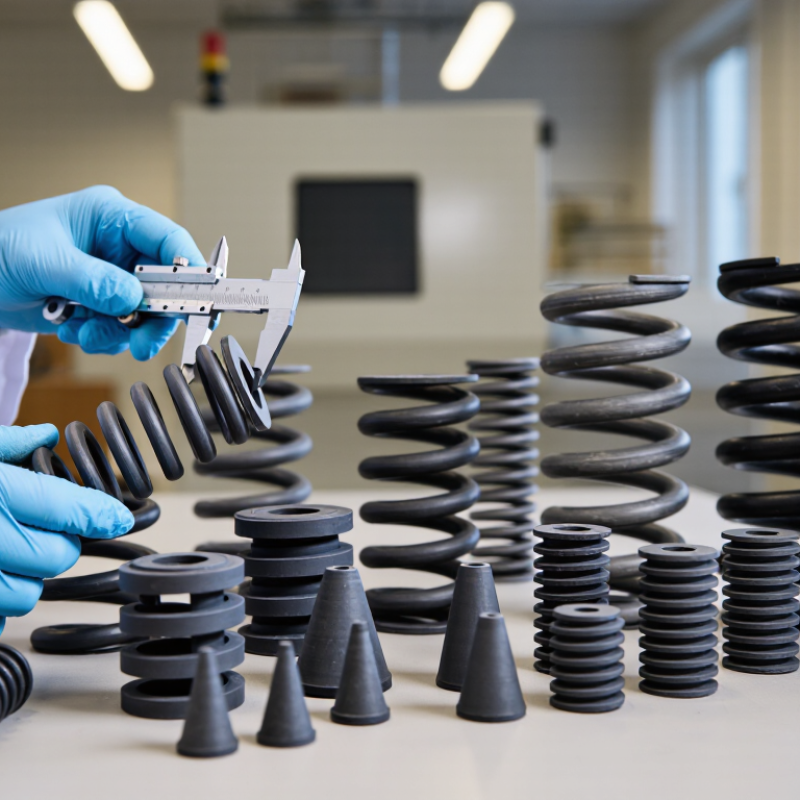
| Dimensional Design | Spring geometry should define outside diameter, inside diameter, free height, end configuration, load direction, and allowable deflection. | ISO 3302-1 provides dimensional tolerance classes for moulded solid rubber products. | Drawing revision, nominal dimensions, tolerance class, concentricity, flatness, and measured dimensional results. | Controlled engineering drawing, inspection plan, first-article report, and calibrated measurement records. | Critical |
| Load and Deflection Performance | Load-deflection behavior should be verified at the specified displacement, loading rate, temperature, and installation condition. | Testing is normally defined by the customer specification or validated internal method; compression testing principles may be based on ASTM D575. | Load at defined deflection, stiffness curve, hysteresis, permanent set, and acceptance limits. | Force-displacement curves, test-fixture drawings, equipment calibration records, and sample identification. | Critical |
| Hardness Control | Rubber hardness must remain within the approved compound and product specification because it directly affects spring rate and load capacity. | ASTM D2240 or ISO 7619-1 for hardness measurement using a durometer. | Shore A hardness, measurement locations, conditioning time, number of readings, and permitted variation. | Batch test report, durometer calibration certificate, and retained reference samples where required. | High |
| Tensile and Elongation Properties | Material strength and extensibility should be suitable for compression, shear, handling, and any combined-load condition. | ASTM D412 or ISO 37 for tensile strength, elongation at break, and related tensile properties. | Tensile strength, elongation at break, specimen type, test speed, conditioning, and failure mode. | Laboratory test report linked to the compound batch and applicable material specification. | High |
| Compression Set | Low compression set is important when the rubber spring must maintain sealing force or load recovery after long-term compression. | ASTM D395 or ISO 815-1 for compression-set testing. | Compression-set percentage, test method, temperature, duration, specimen dimensions, and recovery period. | Routine batch results and separate validation data at the customer’s specified temperature and duration. | High |
| Thermal Aging | Accelerated aging should confirm retention of hardness, tensile strength, elongation, dimensions, and load performance after heat exposure. | ASTM D573 or ISO 188 for accelerated aging in air ovens. | Change in hardness, tensile strength, elongation, mass, dimensions, and load-deflection performance. | Before-and-after test comparison, aging profile, oven calibration, and defined acceptance criteria. | High |
| Fluid Compatibility | Where exposure is expected, the compound must be validated against oils, fuels, hydraulic fluids, coolants, cleaning agents, or other specified media. | ASTM D471 or ISO 1817 for determining the effect of liquids on vulcanized rubber. | Volume change, mass change, hardness change, tensile-property change, swelling, cracking, and visual condition. | Fluid list, exposure conditions, test photographs, post-exposure measurements, and material compatibility statement. | Application-Based |
| Ozone and Weather Resistance | Outdoor or exposed applications should evaluate ozone cracking and weathering resistance using the actual compound and surface condition. | ASTM D1149 or ISO 1431-1 for ozone resistance of vulcanized rubber. | Ozone concentration, exposure duration, strain condition, temperature, crack rating, and visual inspection results. | Ozone-test report, environmental chamber calibration, and defined visual acceptance criteria. | Application-Based |
| Dynamic Fatigue | Repeated compression, shear, or combined loading should be tested to represent the expected service cycle and installation constraints. | Use a documented, validated fatigue method agreed by the buyer and manufacturer; the method must reflect the actual load spectrum. | Cycle count, load loss, stiffness change, crack growth, temperature rise, permanent deformation, and failure mode. | Fatigue protocol, fixture validation, cycle data, failure analysis, and representative production samples. | Critical |
| Moulding Process | Compression, transfer, or injection moulding parameters should be controlled for temperature, pressure, cure time, venting, and cavity consistency. | Process controls should be documented within the supplier’s quality-management system, commonly aligned with ISO 9001. | Mould temperature, cure time, pressure, cavity number, flash level, cure-state verification, and process deviations. | Process-control plan, mould-maintenance records, parameter logs, and nonconformance procedures. | Critical |
| Bonding and Inserts | Metal or polymer inserts require controlled surface preparation, adhesive application, positioning, cure, and bond-strength verification. | Use a validated customer or supplier method for bonded assemblies; inspection criteria should be included in the product specification. | Insert material, coating, surface preparation, adhesive lot, bond-line condition, pull or torque strength, and failure mode. | Bonding work instruction, adhesive traceability, surface-treatment records, and destructive validation results. | Application-Based |
| Surface and Visual Inspection | Finished springs should be free from critical cracks, cuts, blisters, foreign material, exposed reinforcement, severe mould damage, and unacceptable flash. | ISO 3302-1 may support dimensional tolerance selection; visual limits should be defined by an approved inspection standard or drawing. | Defect type, defect size, location, flash height, surface condition, colour uniformity, and disposition status. | Visual inspection standard, operator training record, lighting requirements, defect samples, and inspection checklist. | High |
| Traceability | Every production lot should be traceable to the compound batch, mould, machine, production date, operator, inspection results, and shipment records. | Traceability procedures should be defined within the supplier’s documented quality-management system, commonly aligned with ISO 9001. | Lot number, compound batch, mould cavity, production date, inspection status, and packaging identification. | Digital or paper traceability records retained for the period agreed in the purchase contract. | Critical |
| Measurement System Control | Gauges and test equipment must be suitable for the tolerance and performance range, regularly calibrated, and protected from unauthorized adjustment. | ISO 9001 quality-system requirements and ISO/IEC 17025 principles are commonly used for laboratory competence and calibration control. | Calibration status, measurement uncertainty, gauge repeatability, reproducibility, and equipment identification. | Calibration certificates, measurement-system studies, laboratory scope, and corrective-action records. | High |
| Nonconforming Product Control | Defective material and finished products should be identified, segregated, reviewed, and dispositioned to prevent unintended shipment. | ISO 9001 provides a recognized framework for control of nonconforming outputs and corrective action. | Nonconformance code, quantity affected, root cause, containment action, corrective action, and effectiveness verification. | 8D or equivalent corrective-action report, quarantine records, rework authorization, and closure evidence. | High |
| Pre-Shipment Inspection | Final release should confirm product identity, quantity, dimensions, appearance, packaging, labelling, and all agreed performance checks. | Inspection sampling should be agreed in the purchase specification; statistical sampling may reference ISO 2859-1 when applicable. | Inspection level, acceptance quality limit, sample size, pass/fail results, shipment quantity, and release authorization. | Final inspection report, certificate of conformity, packing list, photographs, and retained samples where required. | Critical |
| Packaging and Storage | Packaging should protect rubber springs from ozone, ultraviolet exposure, heat, contamination, deformation, and excessive compression during transport and storage. | Storage conditions should follow the agreed product specification and recognized rubber-storage practices; packaging requirements should be documented contractually. | Storage temperature, humidity limits, shelf-life date, packaging material, stacking method, and FIFO controls. | Packaging specification, storage instruction, shelf-life declaration, and shipment-condition records. | High |
| Environmental and Regulatory Compliance | Material declarations and restricted-substance controls should match the destination market and the application’s regulatory requirements. | Applicable requirements may include REACH and RoHS for relevant products and markets; applicability must be confirmed for the specific use. | Substance declaration, supplier material disclosure, restricted-substance screening, and compliance status. | Signed compliance declaration, supporting laboratory report where required, and change-notification procedure. | Application-Based |

 Your message must be between 20-3,000 characters!